How to Choose a Vertical Machining Center
Choosing a Vertical Machining Center is not a specification contest. It is a production decision that affects cycle time, part accuracy, tooling costs, and operator workload. Start with the parts you actually make: their dimensions, materials, tolerances, and annual quantities. A small aluminum housing may need high spindle speed and quick tool changes. A steel component with deep pockets may demand torque, rigidity, and dependable chip evacuation. The difference matters.
Manufacturing-systems scholar Yoram Koren’s work emphasizes matching production equipment to changing manufacturing needs. A concise paraphrase of that principle is: “Choose the machine for the production system you need, not for specifications alone.” Treat it as a guide, not a direct quotation. Then compare travels, spindle power, tool capacity, control features, and available floor space against your real jobs. Ask suppliers to demonstrate representative parts, not just showcase cuts. Bring drawings and realistic cycle-time targets.
Look beyond purchase price. Check service response, spare-parts access, training, and the cost of workholding and probing. A larger table can be useful, but it does not automatically improve throughput. Nor does a faster spindle fix poor process planning. Small details count: the tool changer’s reach, coolant delivery into a deep cavity, or room to open the enclosure. I would still question any recommendation based on one impressive sample part. It may not reflect your daily mix. The right Vertical Machining Center should fit today’s workload while leaving sensible room for tomorrow’s. A perfect forecast is unlikely. Plan carefully, then verify the assumptions.
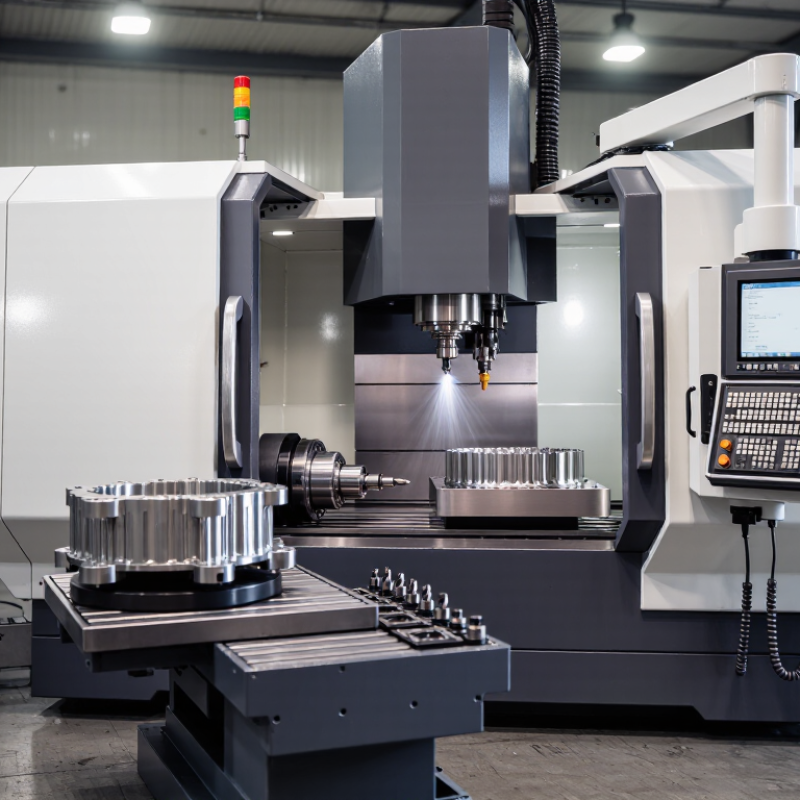
Define the Workpieces and Machining Requirements
How to Choose a Vertical Machining Center
Define the Workpieces and Machining Requirements
Start with the parts you actually expect to make, not an idealized future job. Record each workpiece’s material, overall dimensions, weight, and typical batch size. A compact aluminum housing may need fast tool changes and clear access to several faces. A thick steel plate may demand more cutting force, rigid fixturing, and careful control of heat. These differences matter. If parts vary widely, list the largest and heaviest examples; they often reveal limits that smaller samples hide.
Write down the required tolerances, surface finishes, and features, such as deep pockets, tapped holes, or angled surfaces. Then consider how the part will be held and where tools must reach. A long tool can clear a tall fixture, but it may also deflect during cutting. Be realistic about production volume, too: a setup that works for five parts may slow down a run of five hundred. It is tempting to choose extra capacity “just in case,” yet that can raise purchase and operating costs. Some requirements will change. Mark uncertain ones, check them against actual drawings and cutting trials, and avoid treating guesses as specifications.
Compare Machine Size, Travel, and Load Capacity
Choosing a vertical machining center starts with the part, not the machine’s exterior dimensions. Measure the largest workpiece, then allow room for the vise, fixture, and tool changes. A compact machine may fit the shop floor but leave little space for safe loading. Check doorways, ceiling height, and access for maintenance, too. Small details matter.
Compare X, Y, and Z travel with the full machining setup in place. A part may fit on the table yet exceed usable travel once clamps or a tall fixture are installed. Leave clearance for the spindle nose and tools, especially when drilling deep features. I would double-check the maker’s travel diagram against the actual setup; published numbers can be easy to misread.
Load capacity needs the same careful comparison. Confirm the table’s rated load, and include the workpiece, fixture, vise, and any additional tooling. A heavy part positioned off-center can create concerns that its weight alone does not show. Ask how the rating applies to distributed or concentrated loads. Don’t guess. Also consider how the part will be lifted onto the table. A machine that handles the weight but blocks practical loading may slow every job. That trade-off is worth admitting.
Assess Spindle, Tooling, Accuracy, and Control Options
A vertical machining center should match the parts you actually make, not just the numbers on a specification sheet. Check spindle speed and torque against your materials and cutting tools. Aluminum often benefits from higher speed, while tougher alloys may need stronger low-speed cutting. Ask how the spindle handles sustained loads, not only brief tests. A specification sheet can make this choice look simpler than it is.
Tips: List your most common tools and heaviest cuts before comparing machines. Check tool capacity, change time, and holder compatibility. A crowded magazine can slow a job.
Accuracy depends on more than a stated positioning figure. Consider repeatability, thermal stability, axis travel, and the machine’s performance after warm-up. If parts need tight tolerances, ask for test results under conditions similar to your work. Probe systems can help verify setups, but they do not replace good fixturing or inspection. The control should make common tasks clear: editing offsets, recovering from an interruption, and running programs safely. Have an operator review the interface; a control that seems intuitive in a demo may feel different during a busy shift. Also confirm that your existing programming workflow can support the machine.
Review Automation, Maintenance, and Service Support
When comparing vertical machining centers, review automation as part of the whole production cell, not as an isolated feature. Check whether the machine can support a pallet changer or robot interface, and ask how operators recover from a missed pick or interrupted cycle. Small details matter. For example, a clear access route to the tool magazine can make routine checks less awkward. Confirm that guarding, controls, and operator training match your actual workflow. Automation may raise output, but only when loading, setup, and recovery are planned well.
Maintenance needs equal attention. Ask how technicians reach filters, lubrication points, chip conveyors, and electrical cabinets. A machine that is difficult to clean may lose valuable time between jobs. Request the maintenance schedule and sample service records, then compare them with the hours and materials your shop expects to run. Keep it practical. If the schedule assumes ideal conditions, ask what changes when coolant carries more fines or chips build up during a long run.
Service support can matter most when production stops. Ask about response times, local technician availability, spare-part access, and remote troubleshooting procedures. Find out what training is included and whether your team can get help after installation. A polished service promise is not enough; request clear terms in writing. One caveat: even strong support cannot prevent every delay, and remote diagnosis sometimes misses a problem that only appears at the machine. Be honest about your shop’s limits, too. A complex automated cell may demand more maintenance skill than your current team has.
How to Choose a Vertical Machining Center
Suggested evaluation weights for automation, maintenance, and service support
Use these suggested weights as a starting point when comparing machines. Prioritize maintenance access and service coverage, then adjust the weighting to match your production needs and verify support commitments with each supplier. These are planning guidelines, not survey results.
Calculate Total Ownership Costs and Verify Supplier Fit
A vertical machining center’s price is only the opening line in the budget.
Add freight, rigging, floor preparation, electrical work, coolant equipment, workholding, cutting tools, training, and financing. Small items add up. Estimate costs over several years, not just the first production run. Use cycle times from representative parts, and include setup and changeover time. A fast spindle matters less if fixtures take hours to change.
Ask suppliers to explain what is included in installation and operator training. Confirm service response times, spare-parts availability, and travel charges in writing. Then check those claims with customers running similar materials and shift patterns. A sample cut can help, but bring your own part, tooling, and acceptance criteria. Watch how the supplier handles questions when results differ from the estimate.
Compare expected maintenance, energy use, tool consumption, and unplanned downtime across each option. Downtime costs more. A spreadsheet will still miss something, especially when production schedules change. I may be weighting service too heavily; it depends on whether your team can diagnose faults independently. Check the machine’s work envelope against real fixtures, not just part dimensions, and confirm the supplier can support the control and options your operators will actually use.